Start with the date the goods must be in your hands, then subtract each stage in reverse: delivery, inspection, production, testing, sample approval and design, adding a written buffer to every stage. That is promotional product lead time planning done backward from your event date. For a 15 March 2027 event, the illustrative stage and buffer assumptions below put the latest design start at 22 Dec 2026. Scope: custom promotional products sourced from overseas factories, with assumptions dated 16 October 2026.
Most missed event deadlines are not caused by one dramatic failure. They come from small gaps nobody owned: an artwork file that needed a second round, a sample that waited on a courier, a production slot that moved. Good promotional product lead time planning turns those gaps into visible, owned line items. This guide gives an Operations Manager a repeatable method for turnaround planning, a way to size buffers for sourcing risk, and a delivery contingency you can trigger before the deadline is already lost.
Why Promotional Product Lead Time Planning Works Better in Reverse
Forward planning asks, “When can the supplier finish?” Backward planning asks, “When must we receive the goods, and what has to be true before that?” The second question forces every stage to carry a start date, an owner and a buffer. In promotional product lead time planning, the event date is fixed and everything else is negotiable, so working from the fixed point exposes how much slack you really have.
The method also changes supplier conversations. Instead of asking for one “lead time” figure, you ask for a stage-by-stage quote and compare it with your own timeline. Any stage the supplier cannot describe in writing is a sourcing risk worth flagging early.
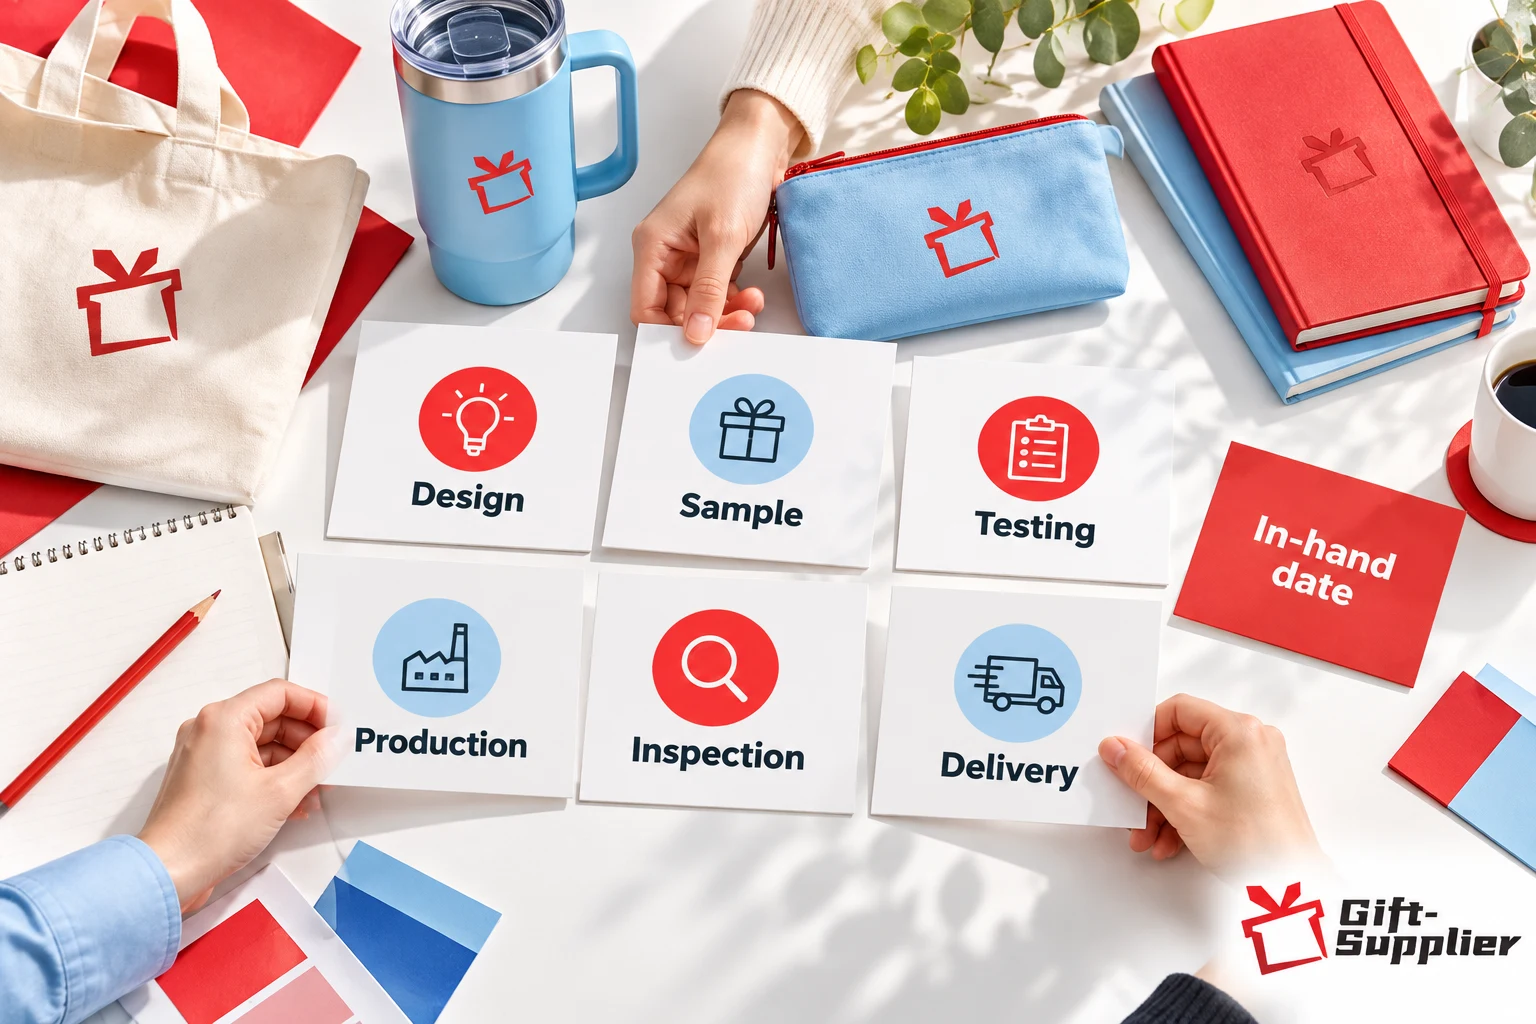
The Six Stages to Map: Design, Sample, Testing, Production, Inspection and Delivery
Before you can build a realistic schedule, name each stage, its decision owner and the evidence that proves it is finished. The table below is the backbone of promotional product lead time planning; durations are deliberately left blank because they must come from a written supplier quote, not from a generic benchmark.
| Stage | What must happen | Decision owner | Evidence of completion | Duration source |
| Design | Artwork, Pantone references and placement approved | Marketing or brand lead | Signed artwork proof | Your team plus supplier design desk |
| Sample | Pre-production sample made and reviewed | Operations Manager | Dated photos and written approval | Supplier quote |
| Testing | Material, safety or function checks that your market requires | Compliance or QC lead | Test report or declaration for the named market | Lab or supplier quote |
| Production | Bulk run against the approved sample | Supplier production manager | Production schedule with start and finish dates | Supplier quote |
| Inspection | Pre-shipment check against an agreed sampling plan | QC lead or third party | Signed inspection report | Inspector or supplier quote |
| Delivery | Freight, customs and last-mile to the venue or warehouse | Logistics owner | Booking confirmation and tracking | Forwarder quote |
Treat each “Duration source” cell as a requirement. If the only source is a verbal estimate, record it as an assumption in your promotional product lead time planning file and widen the buffer.
A Six-Step Framework for Promotional Product Lead Time Planning
Use these steps in order. The decision owner for the whole schedule is the Operations Manager; individual stage owners are listed in Table 1.
- Fix the in-hand date. Agree the date goods must be at the venue or warehouse, not the event day itself.
- List the six stages from Table 1 and remove any that genuinely do not apply, with a note explaining why.
- Collect written durations for each stage from the supplier, lab and forwarder.
- Assign a buffer to each stage using the risk scoring in Table 3.
- Subtract backward from the in-hand date: stage duration plus buffer, one stage at a time, until you reach the latest design start.
- Compare with today’s date. If the gap is negative, choose a delivery contingency from Table 5 now rather than hoping stages compress.
The core formula is: Latest design start = In-hand date − Σ (stage duration + stage buffer). Writing it down matters because it keeps turnaround planning auditable when a stage slips.
Worked example with date-stamped assumptions
The numbers below are illustrative planning assumptions dated 16 October 2026. They are not supplier quotes, market averages or guarantees. Replace them with your own written quotes before you rely on the result. The example assumes calendar days, one factory, one production run and sea or air freight chosen by the forwarder.
| Stage | Duration (days) | Buffer (days) | Window start | Window end |
| Design | 7 | 3 | 22 Dec 2026 | 1 Jan 2027 |
| Sample | 10 | 4 | 1 Jan 2027 | 15 Jan 2027 |
| Testing | 7 | 4 | 15 Jan 2027 | 26 Jan 2027 |
| Production | 21 | 5 | 26 Jan 2027 | 21 Feb 2027 |
| Inspection | 3 | 2 | 21 Feb 2027 | 26 Feb 2027 |
| Delivery | 10 | 7 | 26 Feb 2027 | 15 Mar 2027 |
Added up, stage durations plus buffers total 83 days, so the latest design start is 22 Dec 2026. From 16 October 2026 that leaves 67 days of slack before work must begin. The example also surfaces a real overlap: the production window runs from 26 Jan 2027 to 21 Feb 2027, and published calendars place Lunar New Year in early February 2027. If your factory closes for that holiday, confirm its dates in writing and extend the production buffer accordingly.
Turnaround Planning: How Much Buffer Each Stage Needs
In promotional product lead time planning, a single flat buffer is easy to calculate and usually wrong. A repeat product with an approved sample deserves less protection than a new material with a new print method. Score each stage for novelty, supplier history and external dependency, then size the buffer to match.
| Risk score | Typical situation | Suggested buffer on stage duration | Raise the buffer when |
| Low | Repeat item, approved sample on file, known supplier | 10–15% of stage duration | Any change to material, colour or print method |
| Medium | Repeat supplier, new artwork or colourway | 20–30% of stage duration | Sample is rejected once or approval owner changes |
| High | New supplier, new material, or market-specific testing needed | 35–50% of stage duration | Supplier cannot provide a written stage schedule |
These percentages are a working heuristic for your own planning, not an industry standard. Test them against your last few orders and tune them. The point is consistency: every stage gets an explicit number and a reason for it.
Sourcing Risk Register: Where Promotional Product Lead Time Planning Breaks Down
Sourcing risk rarely announces itself. It appears as a quote that stays vague, a sample that arrives late, or a material substitution mentioned in passing. Use the register below to turn those signals into actions with owners.
| Stage | Early warning signal | Sourcing risk | Action and owner |
| Design | Artwork returned with changes more than twice | Approval loop consumes the buffer | Freeze the artwork version; Marketing lead signs off by a set date |
| Sample | Sample courier date is not confirmed | Approval slides while production slot is held | Ask for dated photos plus a courier booking; Operations Manager |
| Testing | Report names a different material or colour from the order | Test result may not cover the shipped product | Match test sample to bulk spec in writing; QC lead |
| Production | Supplier cannot name a production start date | Slot may be given to another customer | Request a written schedule and a holiday closure list; Operations Manager |
| Inspection | No agreed sampling plan or acceptance criteria | Disputes after goods are packed | Agree sampling method and defect classes before production; QC lead |
| Delivery | Forwarder quote lacks an Incoterms rule | Unclear who carries delay and cost | State the rule in the PO; Logistics owner |
If three or more rows show an active warning signal at the same time, treat the whole plan as high-risk and revisit the buffers in Table 3. Our supplier vetting approach is described on the factory and supply network page, which is the canonical resource for how we qualify and manage factories.
Evidence Block: A Real Quote, Sample and Process Record
This section must hold truthful firsthand evidence before publication. Do not publish invented figures. Use the structure below to insert one anonymised project from your own files, with the buyer context named in general terms (for example, “a regional marketing team ordering event kits”).
| Field | What to insert | Source document |
| Buyer context | Industry, order type, event type (anonymised) | CRM or quote record |
| Planned vs actual dates | Planned and actual start and finish for each stage | Production schedule and inspection report |
| Largest slip | Which stage moved, by how many days, and why | Email trail or QC log |
| Buffer outcome | Whether the buffer absorbed the slip | Project file |
| Lesson learned | One change made to future promotional product lead time planning | Post-project review |
Reviewer note: the author or reviewer confirms in writing that every figure in this section comes from a real file and that the buyer approved its anonymised use.
Delivery Contingency: Choose the Fallback Before the Deadline Moves
A delivery contingency is a pre-agreed fallback, not an emergency improvisation. Decide which option you would use, who authorises it and the trigger date after which it becomes the only viable choice. The table compares common options on criteria a buyer can verify.
| Criterion | Standard freight as planned | Air upgrade | Split shipment | Local top-up stock |
| Effect on lead time | Baseline | Shortens the delivery stage | Part of the order arrives earlier | Fills gap from local supply |
| MOQ impact | None | None | Possible carton and batch limits | Local MOQ may differ |
| Material or spec change | None | None | None | Likely differs from the approved sample |
| Main risk | Late arrival | Freight cost and customs timing | Second shipment slips | Brand mismatch |
| Evidence to request | Booking and schedule | Quote and customs plan | Split schedule per carton | Sample and spec sheet |
| Decision owner | Logistics owner | Operations Manager | Operations Manager | Marketing lead plus Operations |
Cost direction and exact transit times vary by route, season and carrier, so this table avoids universal prices. Get a dated forwarder quote for each option you may need.
Buyer Checklist Before You Confirm the Order
- The in-hand date and venue address are written in the purchase order.
- Every stage has a written duration, a buffer and a named owner.
- The sample approval is dated and signed by the Operations Manager.
- Testing evidence names your target market and matches the bulk specification.
- The supplier has provided a production start date and a holiday closure list.
- Inspection method and acceptance criteria are agreed before production begins.
- An Incoterms rule is stated and the forwarder quote is dated.
- The contingency option and its trigger date are agreed internally.
Risks and Limits of This Approach
- Assumptions are examples. Tables 2 and 3 use illustrative numbers; your suppliers, products and routes will differ.
- Calendar versus working days. Mixing the two is a common error. Choose one convention and state it.
- Market-specific rules. Testing and labelling requirements vary by destination market and change over time; confirm current rules with the relevant regulator before fixing the testing stage.
- Holiday and port disruptions. Closure dates and congestion are volatile and are not predicted by this method.
- No guarantee. Even careful promotional product lead time planning only reduces risk; a buffer does not remove it, and no schedule can promise a delivery date.
Why This Guidance Is Credible
This guide reflects how our operations team applies promotional product lead time planning to orders with factories in our supply network. [Insert author name, role and years of experience in sourcing or production coordination.] The method was reviewed by [reviewer name and role] on 16 October 2026. Insert one sentence naming a real, approved experience claim, such as the number of event orders coordinated, only if it can be verified.
Turn Your Timeline Into a Scoped Quote
Share your event date, product list and target market, and we will return a stage-by-stage timeline you can compare with your own. Request a scoped quote or review how we qualify and manage factories on our factory and supply network page. Send your artwork and spec for a document review before you request samples
Frequently Asked Questions
How early should an Operations Manager start promotional product lead time planning?
Start as soon as the event date and product concept are known. The calculation in Table 2 shows how quickly stage durations and buffers add up, so the later you start, the fewer options remain in Table 6.
Do I need a buffer on every stage?
Yes, but sized to risk. A repeat item with an approved sample can carry a small buffer, while a new material or new supplier needs a larger one. Record the reason for each number.
What if the supplier will only give one total lead time?
Ask for a stage breakdown. If they cannot provide one, treat the total as an assumption and score the sourcing risk as high in your buffer table.
When should I trigger the delivery contingency?
Agree a trigger date in advance, based on the slack left when production should start. Once that date passes without a confirmed production start, move to the pre-selected fallback.
Is testing always required before production?
Not for every product or market. Confirm the requirements for your destination market with the relevant regulator or a qualified lab, then place the testing stage accordingly.
Sources and Further Guidance
International Chamber of Commerce — Incoterms® Rules
US International Trade Commission — Harmonized Tariff Schedule (HTS) search
UK Government — Trade Tariff: look up commodity codes, duty and VAT rates
Author & Reviewer
Written by Claire Morgan, Senior Content Writer, with professional experience modeling inventory and holding costs for promotional programs.
Freshness & Update Log
- Published: October 16, 2026
- Last Reviewed: October 16, 2026
- Next scheduled review: within 12 months, or sooner if cited tariff or freight guidance changes materially.
Related Resources
- /promotional-products-budget-allocation/ — how to decide which portfolio tier a price-break decision should apply to.
- /questions-to-ask-a-promotional-product-supplier/ — 18 evidence-based questions to ask once quotes are in hand.
- /promotional-product-supplier-audit-checklist/ — the 25-point checklist for auditing a supplier before you award the order.
- /promotional-merchandise-vendor-consolidation/ — how vendor consolidation interacts with ongoing performance scoring.