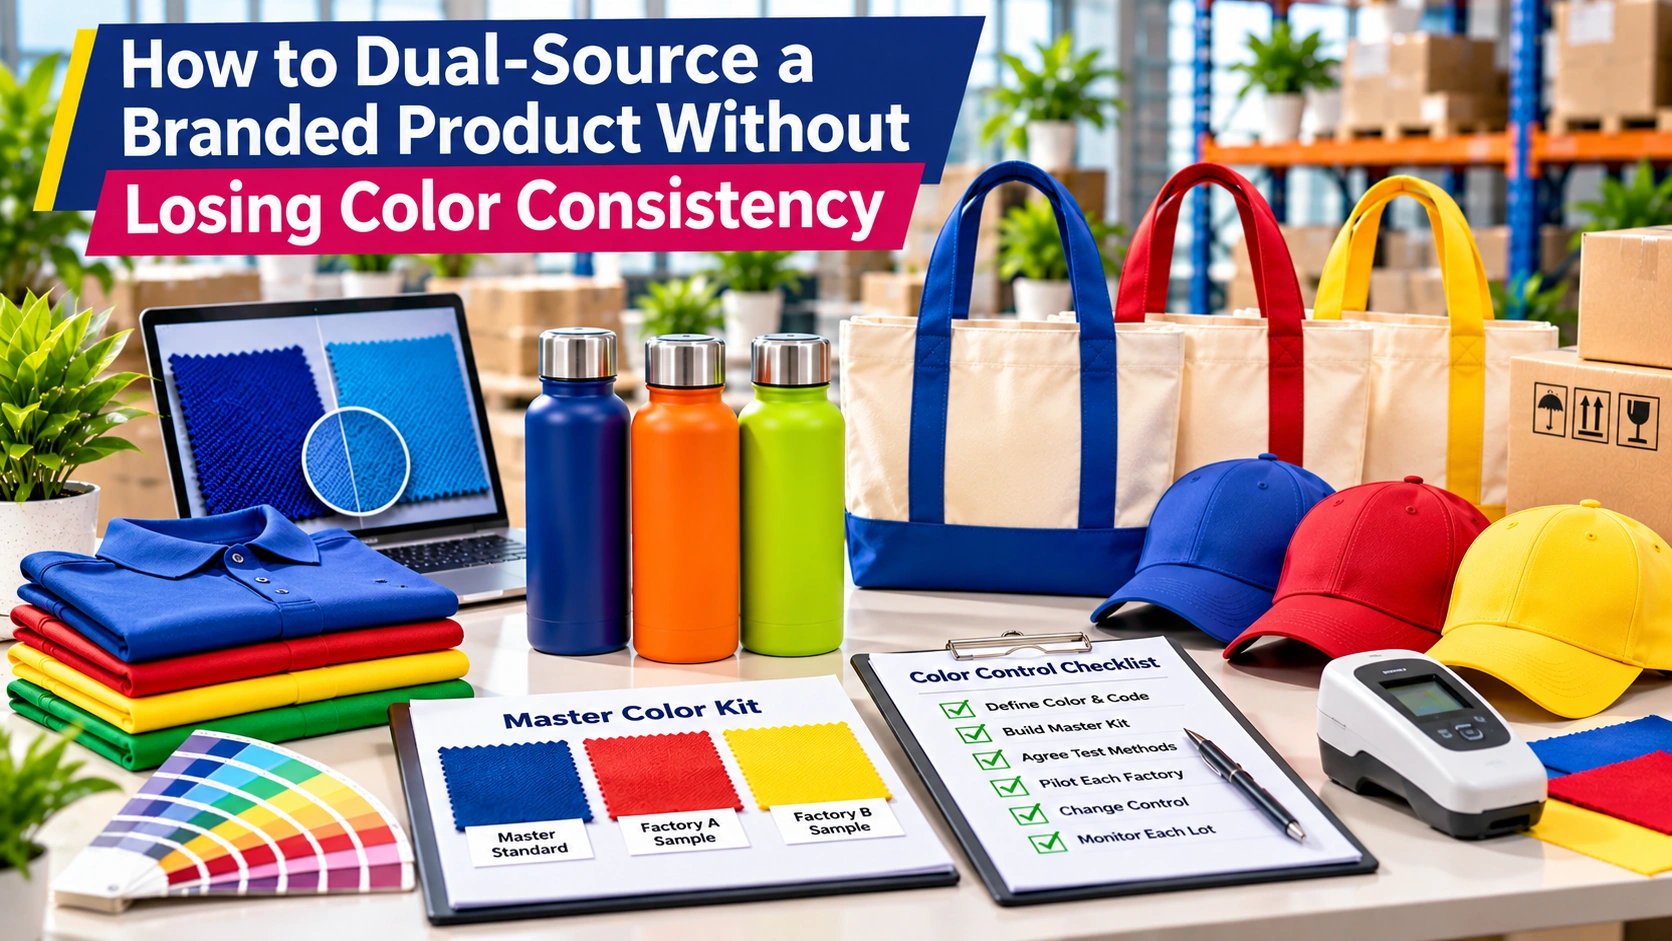
Dual sourcing promotional products without color drift comes down to three controls set before the first order: one master standard that every factory matches, one test method that every factory and your receiving team use to measure it, and one change-control rule that stops any factory altering ink, dye, material or process without written approval. This guide covers color-critical branded items, such as printed or dyed bags, apparel, pens and drinkware, made at two factories for a B2B program. Assumptions are dated 8 November 2026: both factories are qualified, volume is split, and brand colors are defined by reference code and measured values.
If you run operations for a brand program, you probably added a second factory for sound reasons: sourcing risk on a single supplier, tighter turnaround planning, or a delivery contingency for a fixed event date. The catch is that a second factory also brings a second set of inks, dyes, machines and operators, so your brand color now has two interpretations. Buyers rarely see the problem on the purchase order. They see it when cartons from factory A and factory B land in the same warehouse and the logos do not match.
This guide shows how to define the standards, tests and change rules that make dual sourcing promotional products work in practice, so the extra resilience does not cost you brand consistency. It is written for the buyer who is still comparing options, not the buyer ready to place an order.
Why dual sourcing promotional products moves the risk from supply to color
Splitting an order lowers one risk and raises another. A single factory concentrates sourcing risk: one machine breakdown, one shipping delay or one capacity crunch can threaten the whole event date. Two factories spread that risk and give you a genuine delivery contingency. But every shared brand asset now depends on two production processes agreeing with each other, and agreement does not happen by default. A Pantone reference, a PDF artwork file and a verbal instruction to “match the sample” are read differently on different substrates, with different ink systems, on different days.
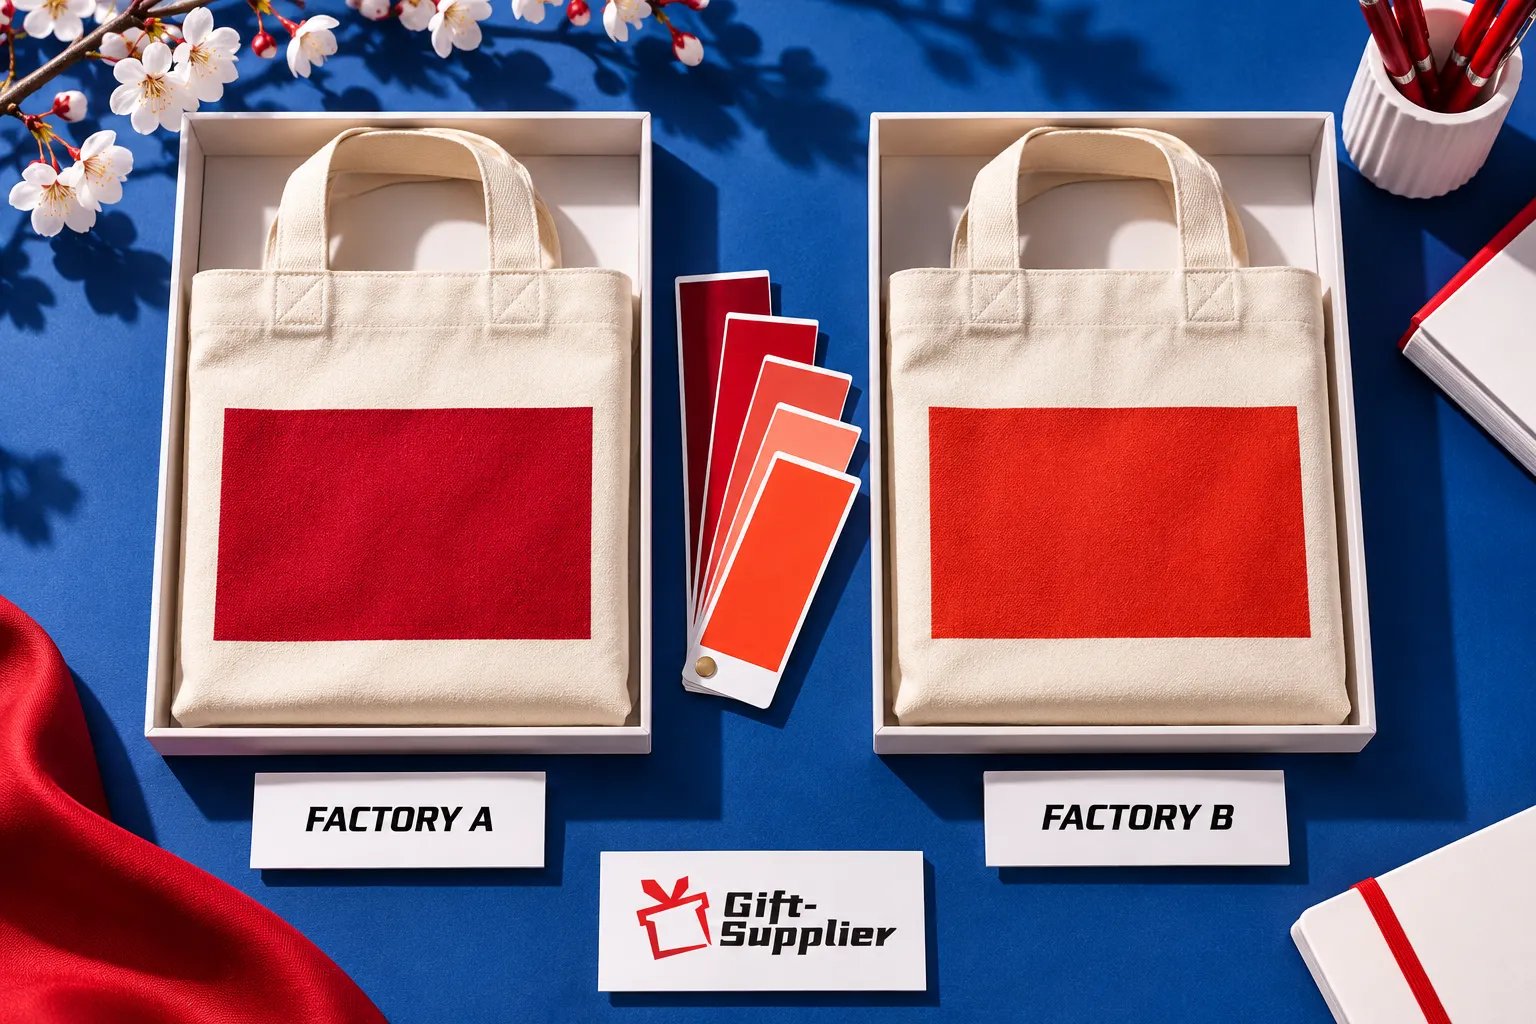
The useful question is therefore not whether to dual source, but which parts of the program need a shared definition of “correct” and which can tolerate variation. A matte black pen barrel tolerates more drift than a brand-red tote bag that will be photographed beside a banner. Treat dual sourcing promotional products as a quality-system decision first and a pricing decision second. Operations owns that decision, with brand and procurement as input, and it should be made before quotes go out, not after the first shipment arrives.
Decision table: single factory, split orders or primary plus qualified backup
Use the table below to compare the three common sourcing models against criteria you can verify in a quote or a sample. It deliberately avoids universal prices and lead times, because both vary by product, material and factory. Capabilities such as audited factory profiles and sample handling are described on our factory and supply network page.
| Criterion | Single factory | Split every order across two factories | Primary factory plus qualified backup |
| Color-match risk | Lowest: one process and one ink or dye system | Highest: two processes on every order, so standards must be tight | Moderate: the backup must match the master only when activated |
| Turnaround planning | One schedule; a slip affects the whole order | Parallel production can shorten the critical path if both start on time | Backup needs a pre-agreed trigger and a short re-qualification window |
| Sourcing risk and delivery contingency | Concentrated in one site | Spread across two sites from day one | Held in reserve; value depends on how recently the backup was tested |
| MOQ and unit cost | One MOQ to meet; verify in the quote | Each factory applies its own MOQ and per-factory quantities fall; verify in both quotes | Backup MOQ applies only if used; confirm any standby or tooling fee |
| Material and process control | One bill of materials | Two bills of materials that must be reconciled | One approved bill of materials plus a mapped equivalent |
| Evidence to request | Pre-production sample and production report | Both factories’ strike-offs against the same master, with measured values | A dated backup pilot on record, with measurements |
| Decision owner | Procurement | Operations manager, with brand approval | Operations manager, with procurement approval |
A six-step framework for dual sourcing promotional products across factories
Work through the steps in order. Each one has a named decision owner, because a standard that nobody owns will drift. The framework answers one buyer question: how do you define master standards, test methods and change control across factories so that two sources behave like one?
Define the color in numbers and in context
Brand manager, with the operations manager. Start with the color definition, not the factory, because dual sourcing promotional products multiplies any ambiguity in it. Record the reference system (for example a Pantone code), the measured L*a*b* values on the real material, the substrate and finish it applies to, and the tolerance you will accept. A Pantone code printed on coated paper looks different on polypropylene or woven cotton, so one code needs one measured target per material family.
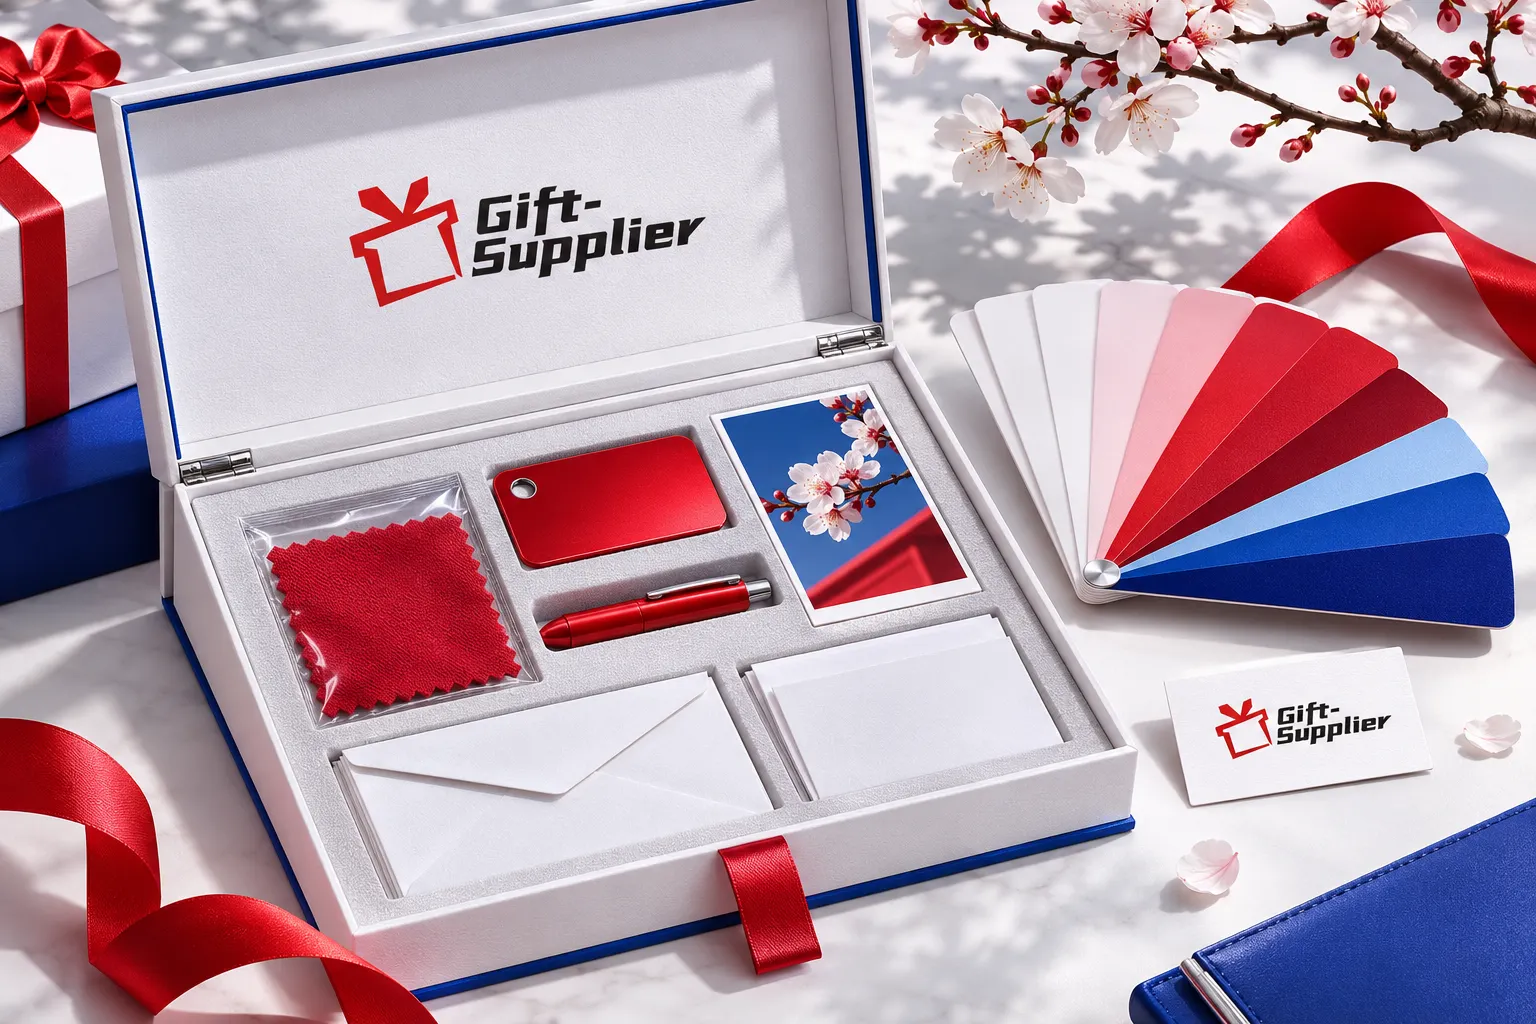
Build a physical master standard kit
Operations manager. The kit is the single reference both factories answer to. It is the cheapest control available for dual sourcing promotional products, and the one most often skipped.
| Element | What to define | Who holds it | How to verify |
| Master color sample | Physical sample on the actual material, sealed and dated, with measured L*a*b* values | Brand owner, with a controlled copy for each factory | Re-measure at set intervals; replace when it fades or wears |
| Approved reference per factory | A signed-off sample from each factory, referenced to the master | Each factory and the buyer | Compare to the master under the agreed light and instrument |
| Decoration specification | Artwork file version, logo size, print method, ink or dye system, placement | Operations manager | Check against the purchase order and approved proof |
| Material specification | Base material, finish, coating and colorant type where relevant | Factory, approved by the buyer | Supplier declaration plus a material check at the pilot |
| Tolerance rule | A limit against the master and a pairwise limit between factories, plus a visual acceptance rule | Brand owner and operations manager | Written into the purchase order and the inspection sheet |
Two details matter most. First, set a pairwise tolerance between factories as well as a tolerance against the master; the worked example later in this guide shows why. Second, retain physical samples from each approved run, because a number without a reference sample cannot settle a dispute.
Agree one set of test methods
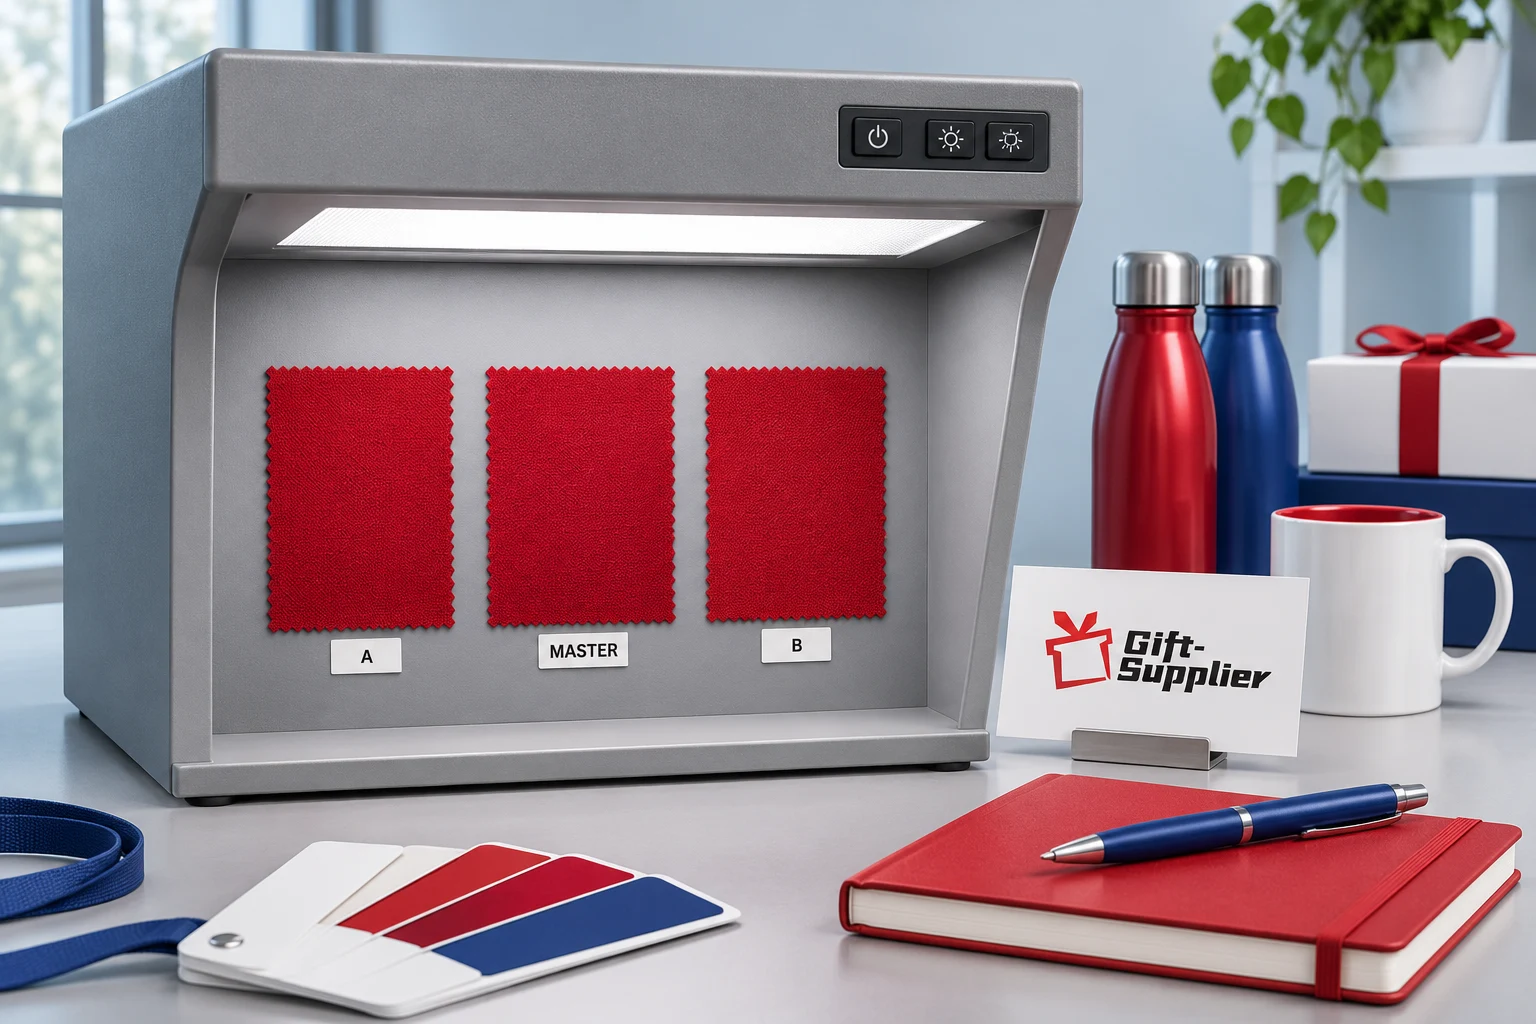
QA lead or operations manager, with each factory’s quality team. In dual sourcing promotional products, both factories and your receiving inspection must measure the same way. Fix the illuminant and observer, the measurement geometry, the instrument (or an agreed offset between instruments), the number of readings per sample and the viewing conditions for the visual check. Where published methods exist, use them instead of house rules, and state the edition you rely on.
| Test | Purpose | Reference to confirm | When | Owner |
| Instrumental color difference (ΔE) | Quantify the distance from the master | ASTM D2244; CIEDE2000 formula (ISO/CIE 11664-6) | Pilot, first article, every lot | Factory QC, verified by the buyer |
| Visual assessment in standard light | Catch what numbers miss, such as metamerism, gloss and texture | ISO 3664 viewing conditions; ASTM D1729 | Pilot and lot release | Operations manager or delegate |
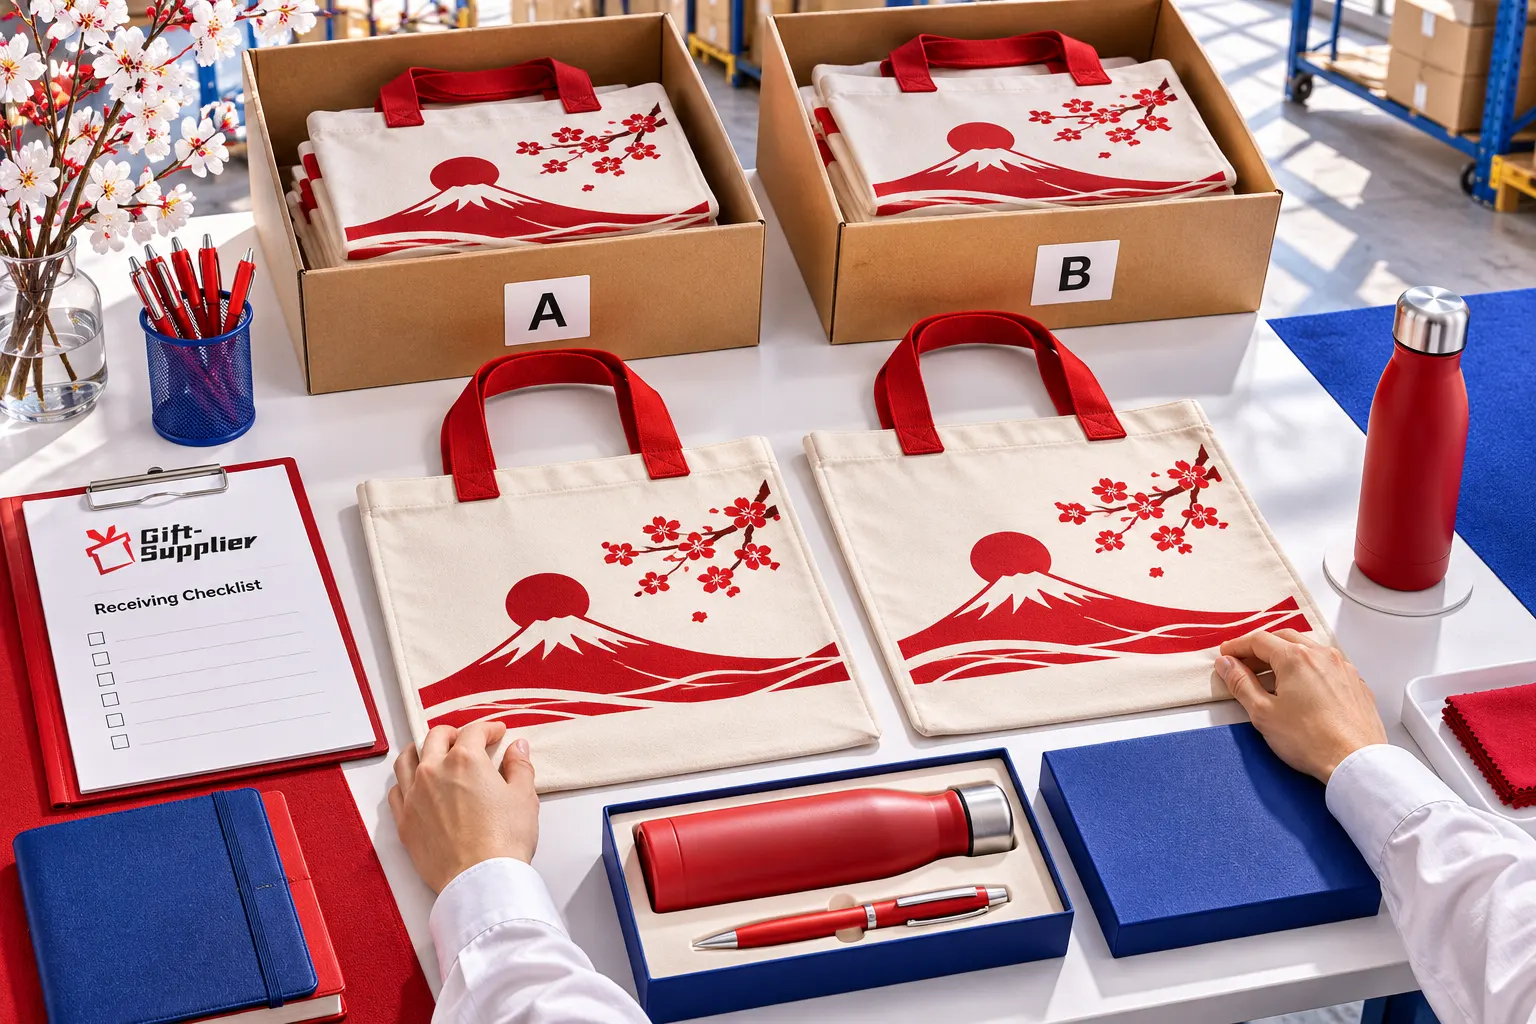
| Side-by-side pairwise check | Confirm items from factory A and B look alike when mixed | Internal procedure using the same booth and instrument | Before each split shipment leaves | Buyer QC or third-party inspector |
| Colorfastness (textiles and similar) | Check dye or print stability under rubbing, light or washing | ISO 105 series, applicable parts | Pilot, and after any material change | Factory lab, spot-checked by the buyer |
| Retained sample comparison | Detect drift over time | Master kit procedure | Each new lot | Operations manager |
Qualify each factory with a pilot run
Operations manager. Qualification for dual sourcing promotional products should prove that each factory can hit the master repeatedly, not that it produced one good sample. Ask each factory for a strike-off or pre-production sample on the real material, measure it with the agreed method, record the result with a date, and only then release volume. A second, independent sample a few days later shows whether the first result was repeatable. If a pilot fails, record the corrective action and re-test rather than loosening the tolerance. Build the pilot into your turnaround planning: sample approval is often the step that quietly consumes the schedule.
Write change control before the first order
Operations manager, with procurement. Most color drift in dual sourcing promotional products after a good pilot comes from changes nobody announced: a new ink or dye supplier, a different base resin, a substituted trim, a moved machine, or a job quietly subcontracted. Define what counts as a change, who must approve it and what evidence closes it.
| Class | Example changes | Rule | Evidence required | Approver |
| A | Operator or shift change; routine maintenance | Notify only | Mention on the next production report | Operations manager (informed) |
| B | New colorant batch from the same supplier; ink formulation adjustment; new print screen | Approve before production | Fresh measurement against the master and a pairwise check | Operations manager |
| C | New colorant or material supplier; different decoration method; new facility or subcontractor | Re-qualify before production | Full pilot with measurements and a new retained sample | Operations manager and brand owner |
Write these rules into your supplier agreement or quality schedule, and ask your legal adviser how to make them enforceable in the jurisdictions involved.
Plan allocation, turnaround and delivery contingency
Operations manager. Dual sourcing promotional products only delivers a delivery contingency if the response is decided before the problem occurs. Agree the triggers and the fallback in advance, and name who can approve each move. For the schedule logic behind these triggers, see the related guides listed at the end of this article, and for how factories are selected and audited, see our factory and supply network overview.
| Scenario | Trigger | Planned response | Decision owner |
| Both factories on schedule | Production reports confirm release dates | Ship as planned; run the pairwise check before consolidating cartons | Operations manager |
| One factory slips | A milestone is missed by an agreed threshold | Move the remaining quantity to the other factory only if its tolerance record and capacity allow; flag mixed-lot risk to the brand owner | Operations manager; brand owner informed |
| One lot fails the color check | Measurement falls outside tolerance | Hold the lot, request corrective action, then choose rework, segregated use with brand approval, or reallocation | Operations manager and brand owner |
| Both factories at risk | A shared material, port or carrier problem | Activate the event-date fallback agreed in advance, such as staged delivery or a substitute item | Operations manager with procurement |
Evidence: why passing against the master is not enough
The calculation below is an illustrative example using assumed readings, not data from a client program. It demonstrates the logic of dual sourcing promotional products under a shared tolerance. Replace it with an anonymized, truthful project example before publication if one is available. The color difference is calculated as ΔE*ab = √(ΔL*² + Δa*² + Δb*²). This simple formula is used here for transparency; CIEDE2000 weights differences differently and gives different values, so name one formula in the purchase order.
| Sample | L* | a* | b* | ΔE*ab | Result |
| Master standard | 48.0 | 52.0 | 18.0 | n/a | Reference |
| Factory A | 48.9 | 51.0 | 17.4 | 1.5 vs master | Within 2.0 |
| Factory B | 47.2 | 52.9 | 19.0 | 1.6 vs master | Within 2.0 |
| Factory A vs Factory B | n/a | n/a | n/a | 3.0 pairwise | Exceeds a 2.0 pairwise limit |
Both factories pass against the master, yet they sit on opposite sides of it and differ from each other by about 3.0. A buyer who mixes cartons on one shelf sees the pairwise gap, not the gap to the master. The fix is to tighten the limit against the master and to add a pairwise limit, then confirm in each pilot that both factories can achieve it. These tolerance values are examples as of 8 November 2026; your brand owner sets the real limit.
Buyer checklist for dual sourcing promotional products
Use this checklist at the quoting stage of dual sourcing promotional products. If an item cannot be ticked, the program is not yet ready to split volume.
- Brand color defined by reference code and measured L*a*b* values, per material family.
- Physical master sample sealed, dated and copied to each factory.
- Tolerance against the master and a pairwise tolerance written into the purchase order.
- One formula, illuminant, observer and measurement geometry named in writing.
- Viewing conditions fixed for visual checks, with a named owner for the final call.
- Pilot result per factory recorded with a date, plus a retained sample.
- Material and decoration specifications frozen, with change classes A, B and C agreed.
- Trigger-based allocation plan for late or failed lots, with named approvers.
- Pairwise check completed before any split shipment is consolidated.
- Per-factory MOQ and quantity assumptions confirmed in both quotes.
Risks and limits of this approach
- Numbers do not replace eyes. Two samples can match under one light and differ under another (metamerism), and gloss, texture and material change how a color looks. Use both instrument and visual checks.
- Tolerances are starting points, not standards. The right limit depends on the product, the material and the brand. Tighter limits can raise rejection rates and cost, so confirm achievability with both factories in the pilot.
- Some items will not match across factories. Different base materials or decoration methods can make a shared master impractical in dual sourcing promotional products. For those items, define separate masters or keep them with one factory.
- Instruments disagree. Different models, calibration states and geometries produce different readings, so agree an offset or use one reference instrument.
- Dual sourcing does not remove every sourcing risk. A shared upstream material, port or carrier problem can affect both factories at once.
- Scope is limited. This guide covers color consistency for branded B2B items as of 8 November 2026. It does not cover chemical restrictions, safety testing or environmental claims, which need separate compliance review.
Why you can rely on this guide
The steps above reflect how multi-factory programs are managed in practice: define the target, share one reference, measure the same way, qualify before releasing volume, and control changes. Our team documents these controls for buyers who rely on dual sourcing promotional products and need two sources to behave as one.
Scope your two-factory plan
To plan dual sourcing promotional products, send your master sample, target quantity, event date and the two factory regions you are considering, and we will respond with a scoped plan that states assumptions, per-factory MOQ and sample steps.
Share your current color standard or purchase order terms for a document review before you commit volume.
Frequently asked questions
How many factories should a branded program use?
For dual sourcing promotional products, two qualified factories is enough to create a real delivery contingency. A third adds coordination and quality-control effort, and is worth considering only when volume, geography or risk justifies it. Verify with quotes from each source.
What color tolerance should we specify?
There is no universal number. Treat any figure you see quoted as a starting point to test in the pilot. Agree the limit with your brand owner, set a limit against the master and between factories, and confirm both factories can meet it on the real material.
Can we split an order if the factories use different decoration methods?
For color-critical items, avoid it where possible. If it is unavoidable, define a separate master for each method, and make sure the two versions are not displayed or kept together.
Who should own change control, us or the factory?
Both. The factory must report changes, and the buyer approves them by class. Without a named buyer-side owner, small changes go unreported until the color has already moved.
How does dual sourcing promotional products affect MOQ and unit cost?
Each factory applies its own MOQ, and splitting lowers the quantity per factory, so unit cost may change. Do not assume a price; ask for quotes at your actual split. You can request a scoped quote that states per-factory MOQ and sample steps.
Sources and Further Guidance
ISO — ISO 31000:2018 Risk management — Guidelines
US Consumer Product Safety Commission — Children’s Product Certificate
UK Government — Placing Manufactured Products on the Market in Great Britain
International Chamber of Commerce — Incoterms® Rules
Author & Reviewer
Written by Claire Morgan, Senior Content Writer, with professional experience managing supply chain risk for branded merchandise programs.
Freshness & Update Log
- Published: November 8, 2026
- Last Reviewed: November 8, 2026
- Next scheduled review: within 6 months, or sooner if cited standards or compliance guidance changes materially.
Related Resources
- /promotional-products-budget-allocation/ — how to decide which portfolio tier a price-break decision should apply to.
- /questions-to-ask-a-promotional-product-supplier/ — 18 evidence-based questions to ask once quotes are in hand.
- /promotional-product-supplier-audit-checklist/ — the 25-point checklist for auditing a supplier before you award the order.
- /promotional-merchandise-vendor-consolidation/ — how vendor consolidation interacts with ongoing performance scoring.